
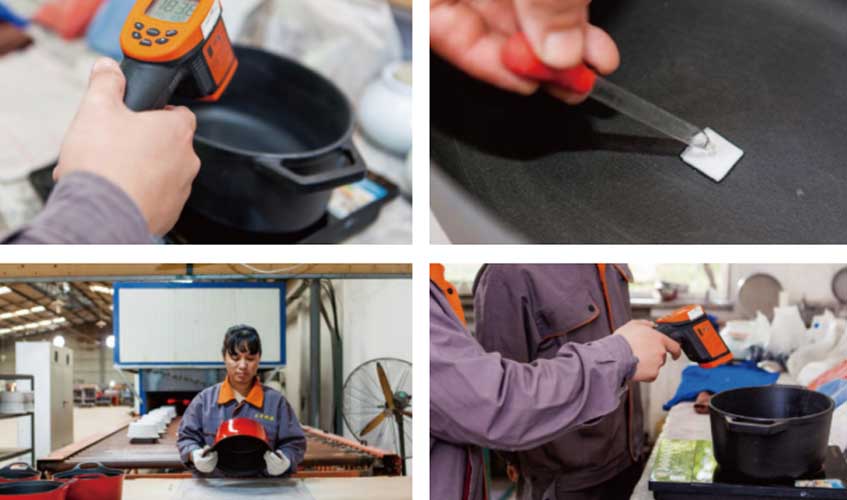
The Precision Manufacturing Process of Enamel Cast Iron Cookware: From Foundry to Kiln
The manufacturing process of enamel cast iron cookware is a sophisticated blend of traditional metallurgy and advanced industrial chemistry. It begins with high-precision casting—often utilizing advanced machine-casting blanks for superior structural tightness and zero deformation—followed by rigorous surface cleaning, the application of independently developed porcelain enamel frits, and high-temperature kiln firing (800°C to 850°C) to permanently fuse the glass glaze to the iron core.
1. Step 1: Pattern Making and Advanced Casting
The quality of any enameled pot starts at the foundry floor, where structural integrity is established:
- Machine-Casting Blanks: Modern, high-end manufacturing utilizes precision machine casting rather than traditional manual pouring alone. This technique provides distinct metallurgical advantages, including stronger metal tightness, exceptional dimensional stability (no deformation), a smoother surface ideal for enamel coating, and secure, reliable delivery timelines.
- Molten Iron Pouring: A carefully balanced iron-carbon alloy is melted down and poured into specialized molds to form the core body of Dutch ovens, skillets, or casseroles.
2. Step 2: Surface Preparation and Shot Blasting
Before any glass can adhere to metal, the raw iron casting must be meticulously prepped:
- Impertinent Cleaning: The rough cast iron blank undergoes mechanical shot-blasting to remove residual sand, microscopic burrs, and surface scale.
- Micro-Texture Profiling: This cleaning creates an optimal microscopic texture across the iron surface, ensuring the liquid or powder enamel coat can lock onto the metal securely during subsequent steps.
3. Step 3: Independent Enamel Frit Development and Application
The heart of enameled cookware lies in the glass coating, known as enamel frit:
- Proprietary Frit Formulation: Leading manufacturers independently develop and formulate their own enamel frits—blends of silica, feldspar, and minerals melted together, quenched, and ground into a fine powder or wet slip.
- Multi-Layer Application: A foundational ground coat is applied first and fired to bond with the iron. Next, colorful exterior glaze layers and smooth interior enamel (such as sand-colored or matte black finishes) are applied uniformly via spraying or dipping.
4. Step 4: High-Temperature Kiln Firing
The final transformation occurs inside massive industrial tunnel kilns:
- Vitreous Fusion: The coated cookware is heated to extreme temperatures ranging between 800°C and 850°C. At this heat, the powdered enamel melts and vitrifies, forming a permanent molecular and mechanical bond with the iron core.
- Quality Inspection: After cooling under controlled conditions, each piece undergoes rigorous quality control checks for enamel thickness, color consistency, and surface perfection before hardware (like stainless steel or phenolic knobs) is attached.
Enamel Cast Iron Production Stages
| Production Stage | Primary Technique / Equipment | Key Engineering Goal |
| 1. Casting | Machine-casting blanks & sand molds | Create a dense, uniform iron body with zero deformation and high tightness. |
| 2. Preparation | Mechanical shot-blasting | Remove casting residue and establish a micro-texture for enamel grip. |
| 3. Enameling | Independent frit formulation & wet/dry application | Apply smooth, non-toxic porcelain layers (ground coat + color/interior coats). |
| 4. Kiln Firing | Industrial tunnel kilns (800°C–850°C) | Permanently fuse the glass enamel to the metal substrate. |
Frequently Asked Questions (FAQ)
Why are machine-casting blanks preferred in cookware manufacturing?
Machine-casting blanks provide superior structural advantages over traditional manual pouring, including stronger metal tightness, resistance to warping or deformation, a smoother surface profile for flawless enamel adherence, and consistent production output.
What is an enamel frit?
An enamel frit is a specialized glass compound made from minerals like silica, borax, and feldspar that are melted at high temperatures, rapidly cooled, and ground into a fine powder or liquid suspension. This is what coats and protects the iron core.
How does high-temperature kiln firing bond the enamel to the iron?
During firing at temperatures between 800°C and 850°C, the glass frits melt and flow into the microscopic pores of the shot-blasted cast iron, creating a permanent chemical and mechanical fusion once cooled.
Does the manufacturing process comply with international food safety standards?
Yes. Premium manufacturers ensure that their enamel frits and firing processes are rigorously tested to comply with strict international food-contact safety regulations, such as LFGB (Europe) and California Proposition 65 (USA), guaranteeing zero heavy metal migration.